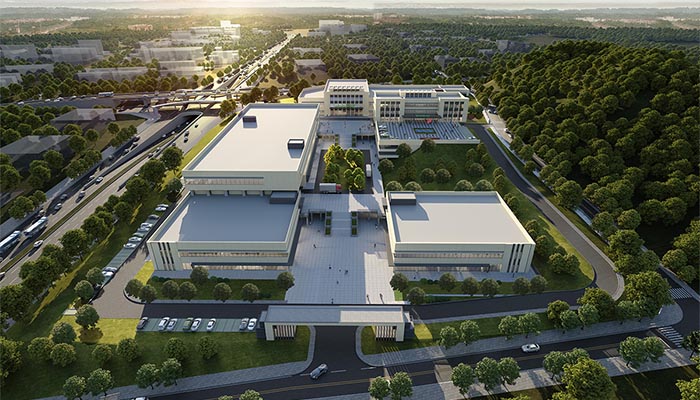
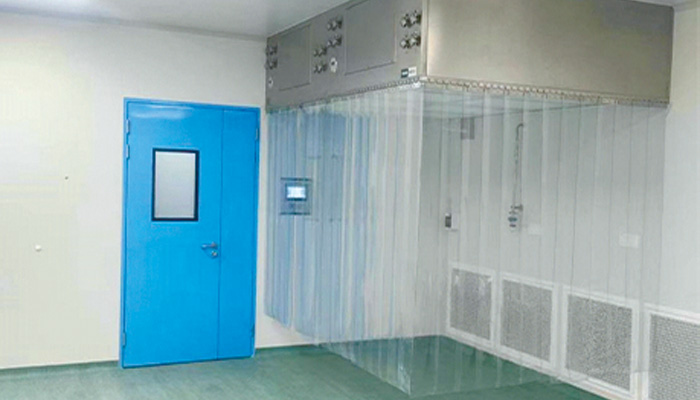
Evaheart Medical — China’s First Artificial Heart Manufacturing Base

Precision Cleanroom Engineering for Implantable Life-Support Devices

Achievement: Supporting the First Clinically Approved & Marketed Implantable Ventricular Assist Device in China

Project Overview

Engineering the Sterile Core for Life-Sustaining Implants

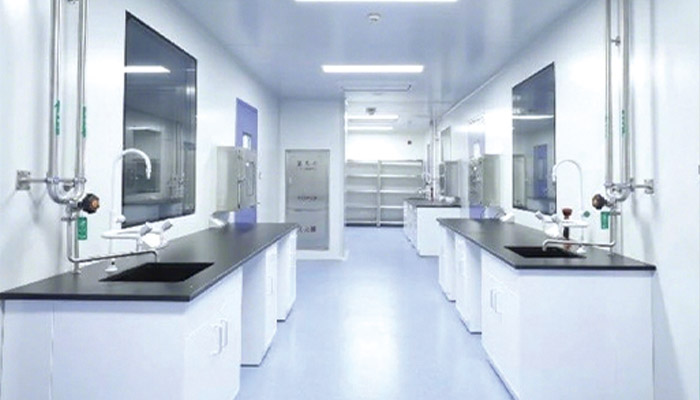
Creating a high-standard cleanroom environment for the production of advanced ventricular assist devices (Artificial Hearts).

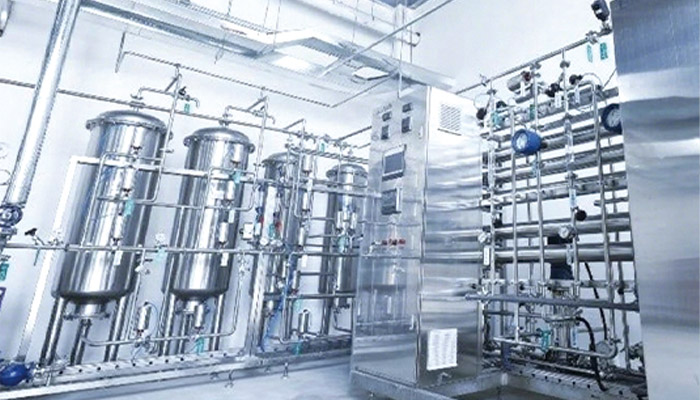
AIPURE delivered the specialized purification infrastructure for Evaheart Medical’s artificial heart production base. Given that these devices are directly implanted into the human body, the manufacturing environment must meet the most stringent sterility and cleanliness benchmarks. Our engineering solution utilizes a sophisticated combination of Constant Air Volume (CAV) and Variable Air Volume (VAV) valve systems to achieve tightly controlled tolerances in environmental regulation. Throughout the project, we provided comprehensive support to ensure the facility achieved full GMP certification for high-end implantable medical device manufacturing.

Technical Highlights

  • Implant-Grade Sterility Standards: Engineered to meet the stringent biological and particulate control requirements for life-sustaining implantable devices.

  • CAV/VAV Hybrid Airflow Control: Deployment of an advanced valve system to maintain a stable pressure cascade and airflow stability across all production zones.

  • Full-Cycle GMP Validation (DQ/IQ/OQ/PQ): Comprehensive management of the Design, Installation, Operational, and Performance Qualification phases to ensure audit-ready compliance.

  • Precision Parameter Regulation: Real-time stabilization of temperature, humidity, and cleanliness to prevent any compromise in product quality.

Engineering Challenges & Solutions

  • Extreme Regulatory Thresholds for Implantable Devices: As products are directly implanted into patients, the facility must operate under fail-safe environmental standards. We designed a high-integrity cleanroom layout that strictly adheres to GMP and industry-specific regulations for sterile medical hardware.

  • Complexity of Airflow Balancing: Achieving a stable pressure gradient while using both fixed and variable air volumes is a major technical hurdle. We integrated precision smart valves to synchronize system linkage, ensuring that pressure remains constant even as production loads fluctuate.

  • End-to-End Validation Management: Meeting GMP standards requires more than just construction; it requires a complete data trail. AIPURE managed the entire verification cycle—from initial design qualification (DQ) to final performance qualification (PQ)—ensuring every system was documented and compliant for official inspection.

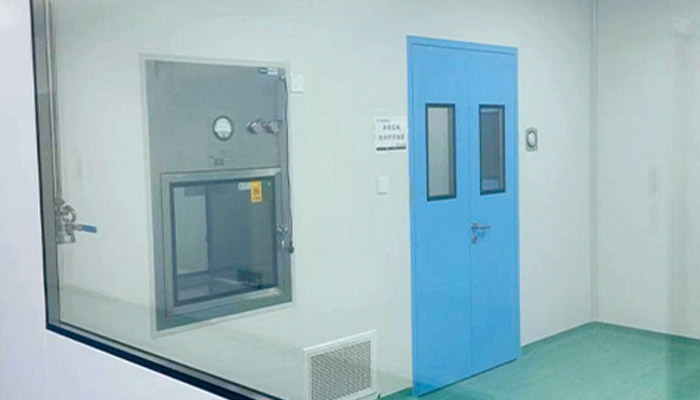
  • Rigorous Contamination & Leakage Control: To guarantee the reliability of the system, we focused on high-integrity airtightness and dust-free construction protocols. Every panel joint and utility penetration was engineered to prevent particulate intrusion, protecting the integrity of the artificial heart assembly process.

Construction Content

  • Implantable Device Assembly Suites: Specialized Grade-A/B cleanrooms designed for sterile mechanical assembly.

  • Intelligent CAV/VAV HVAC Systems: High-precision air handling infrastructure with automated valve regulation.

  • GMP Validation & Documentation Hub: Full-service verification support including DQ, IQ, OQ, and PQ reporting.

  • Integrated Environmental Monitoring (EMS): Digital platforms for continuous tracking of critical airflow and thermal parameters.

Why This Project Defines AIPURE

“Precision engineering for the most delicate rhythms of life.”

The Evaheart project showcases AIPURE’s mastery in “High-Precision Implantable Device EPC.” By successfully integrating complex airflow valve technologies and delivering a facility that passed the most rigorous GMP validation, we prove that our technical standards are capable of supporting the most critical life-saving medical innovations.

Project Conclusion

The high-standard delivery of the Evaheart Artificial Heart production base has provided the client with a world-class facility for life-sustaining medical technology. Our ability to synchronize sophisticated mechanical systems with full GMP compliance ensured that every technical indicator met the design benchmarks for implantable device manufacturing. At AIPURE, we don’t just build cleanrooms; we build the sterile, high-precision foundations that allow medical pioneers to save lives with confidence.

VIEW MORE PROJECTS

Related Service

Cleanroom Consulting

Cleanroom Design

Construction

Product Manufacturing

Commissioning

Operation & Maintain

Contact Information

Global Sales & Technical Support

+86 15607108630

WhatsApp Support

+86 15607108630

China Headquarter Address

No 18 Finance Harbor 4th Road, Wuhan, China.

Request a Tailored Proposal

We respond to technical inquiries within 24 hours.

Scroll to Top