Pharma Cleanroom Solutions: Innovation-Driven Safety
Turnkey EPC for GMP pharmaceutical facilities — from concept design to IQ/OQ/PQ handover, delivered to ISO 14644-1 and EU GMP.
Biopharmaceutical Industry
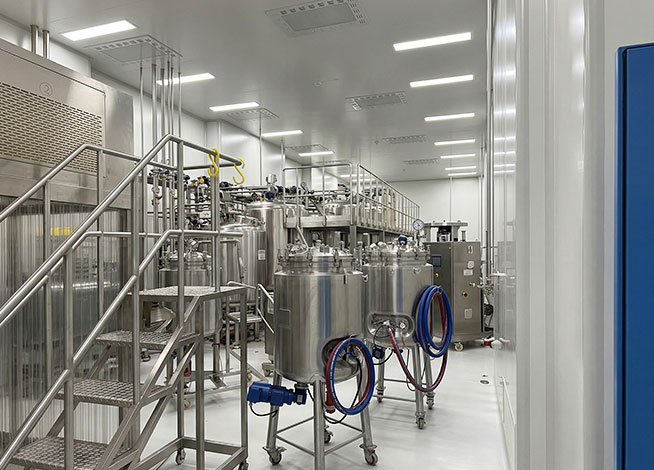
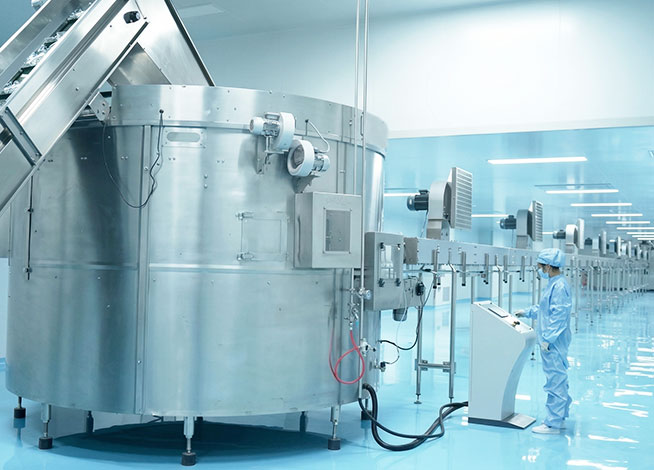
A controlled environment is the primary barrier for safe pharmaceutical production. We focus on microbial and particle contamination control to provide reliable support for R&D and compliant manufacturing.
Cell & Gene Therapy (CGT)
Specialized aseptic processing zones for personalized medicine. Precision pressure cascading and flexible modular layouts to accommodate complex manufacturing workflows.
Vaccine Production
High-containment environments for virus and bacterial handling. BSL-2/BSL-3 compliant facilities with a proven track record of "no reportable biosafety incidents across delivered BSL facilities".
Monoclonal Antibodies (mAbs)
Precision control for large-scale cell culture and purification. Tech Focus: Advanced HVAC systems for constant temperature and humidity, ensuring the stability of biological products.
Chemical Pharmaceutical Industry
We provide comprehensive compliance services that meet FDA, EU, and WHO guidelines, ensuring your chemical drug production is efficient and audit-ready.
Oral Solid Dosage (OSD)
Robust dust containment for tablets and capsules. Cross-contamination prevention through optimized airflow and high-efficiency particle filtration.
Sterile Injectables
Ultra-clean environments for liquid and powder filling. Integration of Barrier Systems (Isolators/RABS) to maintain high-grade aseptic conditions.
API Production (Active Pharmaceutical Ingredients)
Specialized environments for chemical synthesis and crystallization. Solvent-resistant finishes and explosion-proof (ATEX) engineering.
Botanical & Herbal Extraction Facilities
Extraction & Concentration
Humidity-controlled, corrosion-resistant environments for extraction and concentration halls — protecting product integrity throughout solvent recovery and evaporation.
Herbal & Nutraceutical Finished Products
GMP cleanrooms for herbal tablets, powders, capsules, and oral liquids — with microbial load control and automated clean packaging lines.
Pharmaceutical Project References
The AIPURE Advantage
"Productized Engineering" Concept
We utilize a "Productized Engineering" concept to ensure high-quality management and rapid deployment. By standardizing engineering components, we transform complex construction into efficient, intelligent, and ecological assembly.
Regulatory Alignment
Every facility is designed to meet EU GMP, US FDA 21 CFR Part 211, and WHO TRS requirements, with full validation docs. prepared for regulatory audit. NMPA compliance is also available for China-based projects, ensuring your facility is inspection-ready from day one.
End-to-End Validation Support
From initial design and professional engineering management to final validation consulting, we support the high-quality development of the biopharma industry. Across the BSL facilities we have delivered, no biosafety incident has been reported to us by the owner.
H14 HEPA filtration, ≥99.995% efficiency at MPPS per EN 1822-1:2019, installed-leak tested to ISO 14644-3.
Precision HVAC systems providing stable conditions for R&D, production, and storage.
No lost-time safety incidents recorded across 100 delivered BSL and cleanroom projects since 2004.